
Drill Size Chart and Tap Drill Chart
Every number, letter and fractional drill up to 1 inch in size order, metric drills with the nearest inch drill, and tap drills for UNC, UNF and ISO metric threads with the percentage of thread worked out for each.
Standards and method
Number and letter drill diameters are transcribed from ASME B94.11M and cross-checked against a second published table; fractional sizes, millimetres and the percentage of thread are calculated.
Maintained by Miguel Coelho. Updated . See our editorial policy.
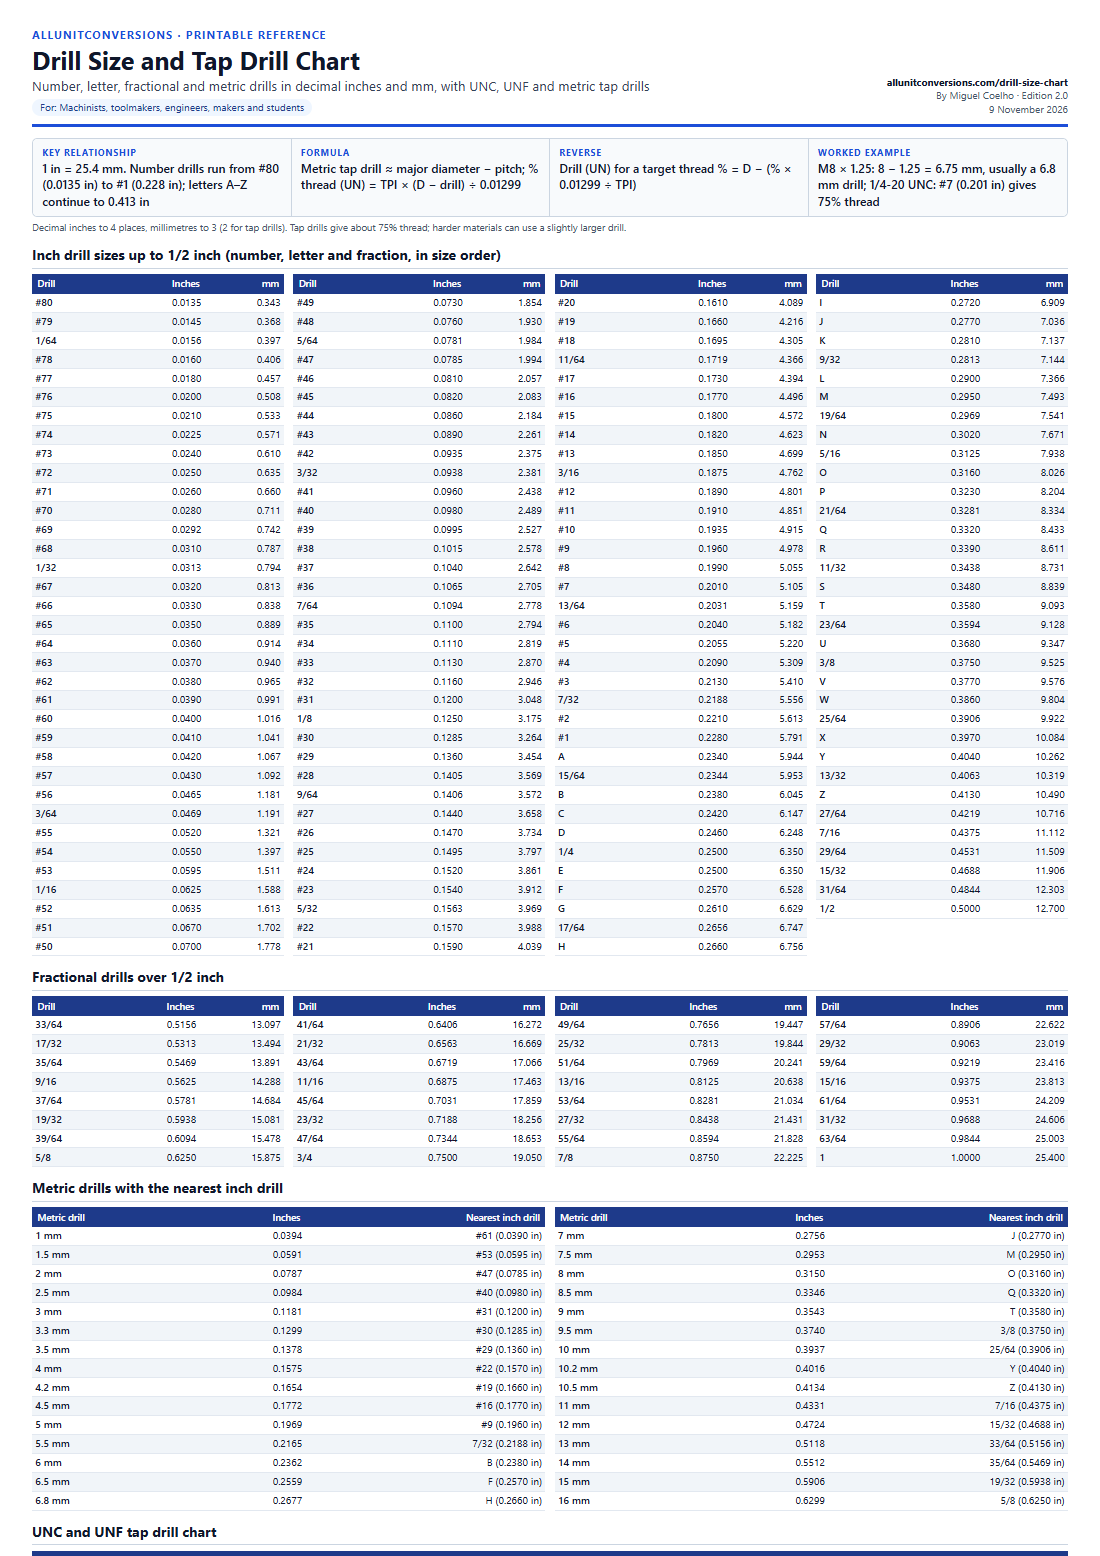
Printable drill size chart
Number, letter, fractional and metric drills in decimal inches and mm, with UNC, UNF and metric tap drills. Includes the exact definition, formulas, a worked example and sources. Conversion values are checked against the defining constants, and reference data is cited to its source, before the PDF is published.
Free to print, share and use in teaching materials with attribution (CC BY 4.0).
Also in the Machinist and Maker Reference Pack, with related sheets in one PDF.
Full drill size chart
Number, letter, fractional and metric drills in decimal inches and mm, with UNC, UNF and metric tap drills. These are the same tables as the printable PDF. For: Machinists, toolmakers, engineers, makers and students.
- Key relationship
- 1 in = 25.4 mm. Number drills run from #80 (0.0135 in) to #1 (0.228 in); letters A–Z continue to 0.413 in
- Formula
- Metric tap drill ≈ major diameter − pitch; % thread (UN) = TPI × (D − drill) ÷ 0.01299
- Reverse
- Drill (UN) for a target thread % = D − (% × 0.01299 ÷ TPI)
- Worked example
- M8 × 1.25: 8 − 1.25 = 6.75 mm, usually a 6.8 mm drill; 1/4-20 UNC: #7 (0.201 in) gives 75% thread
- Rounding
- Decimal inches to 4 places, millimetres to 3 (2 for tap drills). Tap drills give about 75% thread; harder materials can use a slightly larger drill.
Inch drill sizes up to 1/2 inch (number, letter and fraction, in size order)
| Drill | Inches | mm |
|---|---|---|
| #80 | 0.0135 | 0.343 |
| #79 | 0.0145 | 0.368 |
| 1/64 | 0.0156 | 0.397 |
| #78 | 0.0160 | 0.406 |
| #77 | 0.0180 | 0.457 |
| #76 | 0.0200 | 0.508 |
| #75 | 0.0210 | 0.533 |
| #74 | 0.0225 | 0.571 |
| #73 | 0.0240 | 0.610 |
| #72 | 0.0250 | 0.635 |
| #71 | 0.0260 | 0.660 |
| #70 | 0.0280 | 0.711 |
| #69 | 0.0292 | 0.742 |
| #68 | 0.0310 | 0.787 |
| 1/32 | 0.0313 | 0.794 |
| #67 | 0.0320 | 0.813 |
| #66 | 0.0330 | 0.838 |
| #65 | 0.0350 | 0.889 |
| #64 | 0.0360 | 0.914 |
| #63 | 0.0370 | 0.940 |
| #62 | 0.0380 | 0.965 |
| #61 | 0.0390 | 0.991 |
| #60 | 0.0400 | 1.016 |
| #59 | 0.0410 | 1.041 |
| #58 | 0.0420 | 1.067 |
| #57 | 0.0430 | 1.092 |
| #56 | 0.0465 | 1.181 |
| 3/64 | 0.0469 | 1.191 |
| #55 | 0.0520 | 1.321 |
| #54 | 0.0550 | 1.397 |
| #53 | 0.0595 | 1.511 |
| 1/16 | 0.0625 | 1.588 |
| #52 | 0.0635 | 1.613 |
| #51 | 0.0670 | 1.702 |
| #50 | 0.0700 | 1.778 |
| #49 | 0.0730 | 1.854 |
| #48 | 0.0760 | 1.930 |
| 5/64 | 0.0781 | 1.984 |
| #47 | 0.0785 | 1.994 |
| #46 | 0.0810 | 2.057 |
| #45 | 0.0820 | 2.083 |
| #44 | 0.0860 | 2.184 |
| #43 | 0.0890 | 2.261 |
| #42 | 0.0935 | 2.375 |
| 3/32 | 0.0938 | 2.381 |
| #41 | 0.0960 | 2.438 |
| Drill | Inches | mm |
|---|---|---|
| #40 | 0.0980 | 2.489 |
| #39 | 0.0995 | 2.527 |
| #38 | 0.1015 | 2.578 |
| #37 | 0.1040 | 2.642 |
| #36 | 0.1065 | 2.705 |
| 7/64 | 0.1094 | 2.778 |
| #35 | 0.1100 | 2.794 |
| #34 | 0.1110 | 2.819 |
| #33 | 0.1130 | 2.870 |
| #32 | 0.1160 | 2.946 |
| #31 | 0.1200 | 3.048 |
| 1/8 | 0.1250 | 3.175 |
| #30 | 0.1285 | 3.264 |
| #29 | 0.1360 | 3.454 |
| #28 | 0.1405 | 3.569 |
| 9/64 | 0.1406 | 3.572 |
| #27 | 0.1440 | 3.658 |
| #26 | 0.1470 | 3.734 |
| #25 | 0.1495 | 3.797 |
| #24 | 0.1520 | 3.861 |
| #23 | 0.1540 | 3.912 |
| 5/32 | 0.1563 | 3.969 |
| #22 | 0.1570 | 3.988 |
| #21 | 0.1590 | 4.039 |
| #20 | 0.1610 | 4.089 |
| #19 | 0.1660 | 4.216 |
| #18 | 0.1695 | 4.305 |
| 11/64 | 0.1719 | 4.366 |
| #17 | 0.1730 | 4.394 |
| #16 | 0.1770 | 4.496 |
| #15 | 0.1800 | 4.572 |
| #14 | 0.1820 | 4.623 |
| #13 | 0.1850 | 4.699 |
| 3/16 | 0.1875 | 4.762 |
| #12 | 0.1890 | 4.801 |
| #11 | 0.1910 | 4.851 |
| #10 | 0.1935 | 4.915 |
| #9 | 0.1960 | 4.978 |
| #8 | 0.1990 | 5.055 |
| #7 | 0.2010 | 5.105 |
| 13/64 | 0.2031 | 5.159 |
| #6 | 0.2040 | 5.182 |
| #5 | 0.2055 | 5.220 |
| #4 | 0.2090 | 5.309 |
| #3 | 0.2130 | 5.410 |
| 7/32 | 0.2188 | 5.556 |
| Drill | Inches | mm |
|---|---|---|
| #2 | 0.2210 | 5.613 |
| #1 | 0.2280 | 5.791 |
| A | 0.2340 | 5.944 |
| 15/64 | 0.2344 | 5.953 |
| B | 0.2380 | 6.045 |
| C | 0.2420 | 6.147 |
| D | 0.2460 | 6.248 |
| 1/4 | 0.2500 | 6.350 |
| E | 0.2500 | 6.350 |
| F | 0.2570 | 6.528 |
| G | 0.2610 | 6.629 |
| 17/64 | 0.2656 | 6.747 |
| H | 0.2660 | 6.756 |
| I | 0.2720 | 6.909 |
| J | 0.2770 | 7.036 |
| K | 0.2810 | 7.137 |
| 9/32 | 0.2813 | 7.144 |
| L | 0.2900 | 7.366 |
| M | 0.2950 | 7.493 |
| 19/64 | 0.2969 | 7.541 |
| N | 0.3020 | 7.671 |
| 5/16 | 0.3125 | 7.938 |
| O | 0.3160 | 8.026 |
| P | 0.3230 | 8.204 |
| 21/64 | 0.3281 | 8.334 |
| Q | 0.3320 | 8.433 |
| R | 0.3390 | 8.611 |
| 11/32 | 0.3438 | 8.731 |
| S | 0.3480 | 8.839 |
| T | 0.3580 | 9.093 |
| 23/64 | 0.3594 | 9.128 |
| U | 0.3680 | 9.347 |
| 3/8 | 0.3750 | 9.525 |
| V | 0.3770 | 9.576 |
| W | 0.3860 | 9.804 |
| 25/64 | 0.3906 | 9.922 |
| X | 0.3970 | 10.084 |
| Y | 0.4040 | 10.262 |
| 13/32 | 0.4063 | 10.319 |
| Z | 0.4130 | 10.490 |
| 27/64 | 0.4219 | 10.716 |
| 7/16 | 0.4375 | 11.112 |
| 29/64 | 0.4531 | 11.509 |
| 15/32 | 0.4688 | 11.906 |
| 31/64 | 0.4844 | 12.303 |
| 1/2 | 0.5000 | 12.700 |
Fractional drills over 1/2 inch
| Drill | Inches | mm |
|---|---|---|
| 33/64 | 0.5156 | 13.097 |
| 17/32 | 0.5313 | 13.494 |
| 35/64 | 0.5469 | 13.891 |
| 9/16 | 0.5625 | 14.288 |
| 37/64 | 0.5781 | 14.684 |
| 19/32 | 0.5938 | 15.081 |
| 39/64 | 0.6094 | 15.478 |
| 5/8 | 0.6250 | 15.875 |
| 41/64 | 0.6406 | 16.272 |
| 21/32 | 0.6563 | 16.669 |
| 43/64 | 0.6719 | 17.066 |
| Drill | Inches | mm |
|---|---|---|
| 11/16 | 0.6875 | 17.463 |
| 45/64 | 0.7031 | 17.859 |
| 23/32 | 0.7188 | 18.256 |
| 47/64 | 0.7344 | 18.653 |
| 3/4 | 0.7500 | 19.050 |
| 49/64 | 0.7656 | 19.447 |
| 25/32 | 0.7813 | 19.844 |
| 51/64 | 0.7969 | 20.241 |
| 13/16 | 0.8125 | 20.638 |
| 53/64 | 0.8281 | 21.034 |
| 27/32 | 0.8438 | 21.431 |
| Drill | Inches | mm |
|---|---|---|
| 55/64 | 0.8594 | 21.828 |
| 7/8 | 0.8750 | 22.225 |
| 57/64 | 0.8906 | 22.622 |
| 29/32 | 0.9063 | 23.019 |
| 59/64 | 0.9219 | 23.416 |
| 15/16 | 0.9375 | 23.813 |
| 61/64 | 0.9531 | 24.209 |
| 31/32 | 0.9688 | 24.606 |
| 63/64 | 0.9844 | 25.003 |
| 1 | 1.0000 | 25.400 |
Metric drills with the nearest inch drill
| Metric drill | Inches | Nearest inch drill |
|---|---|---|
| 1 mm | 0.0394 | #61 (0.0390 in) |
| 1.5 mm | 0.0591 | #53 (0.0595 in) |
| 2 mm | 0.0787 | #47 (0.0785 in) |
| 2.5 mm | 0.0984 | #40 (0.0980 in) |
| 3 mm | 0.1181 | #31 (0.1200 in) |
| 3.3 mm | 0.1299 | #30 (0.1285 in) |
| 3.5 mm | 0.1378 | #29 (0.1360 in) |
| 4 mm | 0.1575 | #22 (0.1570 in) |
| 4.2 mm | 0.1654 | #19 (0.1660 in) |
| 4.5 mm | 0.1772 | #16 (0.1770 in) |
| 5 mm | 0.1969 | #9 (0.1960 in) |
| 5.5 mm | 0.2165 | 7/32 (0.2188 in) |
| 6 mm | 0.2362 | B (0.2380 in) |
| 6.5 mm | 0.2559 | F (0.2570 in) |
| 6.8 mm | 0.2677 | H (0.2660 in) |
| Metric drill | Inches | Nearest inch drill |
|---|---|---|
| 7 mm | 0.2756 | J (0.2770 in) |
| 7.5 mm | 0.2953 | M (0.2950 in) |
| 8 mm | 0.3150 | O (0.3160 in) |
| 8.5 mm | 0.3346 | Q (0.3320 in) |
| 9 mm | 0.3543 | T (0.3580 in) |
| 9.5 mm | 0.3740 | 3/8 (0.3750 in) |
| 10 mm | 0.3937 | 25/64 (0.3906 in) |
| 10.2 mm | 0.4016 | Y (0.4040 in) |
| 10.5 mm | 0.4134 | Z (0.4130 in) |
| 11 mm | 0.4331 | 7/16 (0.4375 in) |
| 12 mm | 0.4724 | 15/32 (0.4688 in) |
| 13 mm | 0.5118 | 33/64 (0.5156 in) |
| 14 mm | 0.5512 | 35/64 (0.5469 in) |
| 15 mm | 0.5906 | 19/32 (0.5938 in) |
| 16 mm | 0.6299 | 5/8 (0.6250 in) |
UNC and UNF tap drill chart
| Thread | Major dia. (in) | TPI | Tap drill | Drill (in) | Drill (mm) | Thread % |
|---|---|---|---|---|---|---|
| #0-80 UNF | 0.0600 | 80 | 3/64 | 0.0469 | 1.19 | 81% |
| #1-64 UNC | 0.0730 | 64 | #53 | 0.0595 | 1.51 | 67% |
| #1-72 UNF | 0.0730 | 72 | #53 | 0.0595 | 1.51 | 75% |
| #2-56 UNC | 0.0860 | 56 | #50 | 0.0700 | 1.78 | 69% |
| #2-64 UNF | 0.0860 | 64 | #50 | 0.0700 | 1.78 | 79% |
| #3-48 UNC | 0.0990 | 48 | #47 | 0.0785 | 1.99 | 76% |
| #3-56 UNF | 0.0990 | 56 | #45 | 0.0820 | 2.08 | 73% |
| #4-40 UNC | 0.1120 | 40 | #43 | 0.0890 | 2.26 | 71% |
| #4-48 UNF | 0.1120 | 48 | #42 | 0.0935 | 2.37 | 68% |
| #5-40 UNC | 0.1250 | 40 | #38 | 0.1015 | 2.58 | 72% |
| #5-44 UNF | 0.1250 | 44 | #37 | 0.1040 | 2.64 | 71% |
| #6-32 UNC | 0.1380 | 32 | #36 | 0.1065 | 2.71 | 78% |
| #6-40 UNF | 0.1380 | 40 | #33 | 0.1130 | 2.87 | 77% |
| #8-32 UNC | 0.1640 | 32 | #29 | 0.1360 | 3.45 | 69% |
| #8-36 UNF | 0.1640 | 36 | #29 | 0.1360 | 3.45 | 78% |
| #10-24 UNC | 0.1900 | 24 | #25 | 0.1495 | 3.80 | 75% |
| #10-32 UNF | 0.1900 | 32 | #21 | 0.1590 | 4.04 | 76% |
| #12-24 UNC | 0.2160 | 24 | #16 | 0.1770 | 4.50 | 72% |
| #12-28 UNF | 0.2160 | 28 | #14 | 0.1820 | 4.62 | 73% |
| 1/4-20 UNC | 0.2500 | 20 | #7 | 0.2010 | 5.11 | 75% |
| 1/4-28 UNF | 0.2500 | 28 | #3 | 0.2130 | 5.41 | 80% |
| 5/16-18 UNC | 0.3125 | 18 | F | 0.2570 | 6.53 | 77% |
| 5/16-24 UNF | 0.3125 | 24 | I | 0.2720 | 6.91 | 75% |
| 3/8-16 UNC | 0.3750 | 16 | 5/16 | 0.3125 | 7.94 | 77% |
| 3/8-24 UNF | 0.3750 | 24 | Q | 0.3320 | 8.43 | 79% |
| 7/16-14 UNC | 0.4375 | 14 | U | 0.3680 | 9.35 | 75% |
| 7/16-20 UNF | 0.4375 | 20 | 25/64 | 0.3906 | 9.92 | 72% |
| 1/2-13 UNC | 0.5000 | 13 | 27/64 | 0.4219 | 10.72 | 78% |
| 1/2-20 UNF | 0.5000 | 20 | 29/64 | 0.4531 | 11.51 | 72% |
| 9/16-12 UNC | 0.5625 | 12 | 31/64 | 0.4844 | 12.30 | 72% |
| 9/16-18 UNF | 0.5625 | 18 | 33/64 | 0.5156 | 13.10 | 65% |
| 5/8-11 UNC | 0.6250 | 11 | 17/32 | 0.5313 | 13.49 | 79% |
| 5/8-18 UNF | 0.6250 | 18 | 37/64 | 0.5781 | 14.68 | 65% |
| 3/4-10 UNC | 0.7500 | 10 | 21/32 | 0.6563 | 16.67 | 72% |
| 3/4-16 UNF | 0.7500 | 16 | 11/16 | 0.6875 | 17.46 | 77% |
| 7/8-9 UNC | 0.8750 | 9 | 49/64 | 0.7656 | 19.45 | 76% |
| 7/8-14 UNF | 0.8750 | 14 | 13/16 | 0.8125 | 20.64 | 67% |
| 1-8 UNC | 1.0000 | 8 | 7/8 | 0.8750 | 22.22 | 77% |
| 1-12 UNF | 1.0000 | 12 | 59/64 | 0.9219 | 23.42 | 72% |
ISO metric tap drill chart (coarse and fine)
| Thread | Pitch (mm) | Series | D − P (mm) | Usual drill (mm) | Drill (in) |
|---|---|---|---|---|---|
| M1 × 0.25 | 0.25 | Coarse | 0.75 | 0.75 | 0.0295 |
| M1.2 × 0.25 | 0.25 | Coarse | 0.95 | 0.95 | 0.0374 |
| M1.4 × 0.3 | 0.3 | Coarse | 1.1 | 1.1 | 0.0433 |
| M1.6 × 0.35 | 0.35 | Coarse | 1.25 | 1.25 | 0.0492 |
| M2 × 0.4 | 0.4 | Coarse | 1.6 | 1.6 | 0.0630 |
| M2.5 × 0.45 | 0.45 | Coarse | 2.05 | 2.05 | 0.0807 |
| M3 × 0.5 | 0.5 | Coarse | 2.5 | 2.5 | 0.0984 |
| M3.5 × 0.6 | 0.6 | Coarse | 2.9 | 2.9 | 0.1142 |
| M4 × 0.7 | 0.7 | Coarse | 3.3 | 3.3 | 0.1299 |
| M5 × 0.8 | 0.8 | Coarse | 4.2 | 4.2 | 0.1654 |
| M6 × 1 | 1 | Coarse | 5 | 5 | 0.1969 |
| M8 × 1.25 | 1.25 | Coarse | 6.75 | 6.8 | 0.2677 |
| M8 × 1 | 1 | Fine | 7 | 7 | 0.2756 |
| M10 × 1.5 | 1.5 | Coarse | 8.5 | 8.5 | 0.3346 |
| M10 × 1.25 | 1.25 | Fine | 8.75 | 8.8 | 0.3465 |
| M10 × 1 | 1 | Fine | 9 | 9 | 0.3543 |
| M12 × 1.75 | 1.75 | Coarse | 10.25 | 10.2 | 0.4016 |
| M12 × 1.5 | 1.5 | Fine | 10.5 | 10.5 | 0.4134 |
| M12 × 1.25 | 1.25 | Fine | 10.75 | 10.8 | 0.4252 |
| M14 × 2 | 2 | Coarse | 12 | 12 | 0.4724 |
| M14 × 1.5 | 1.5 | Fine | 12.5 | 12.5 | 0.4921 |
| M16 × 2 | 2 | Coarse | 14 | 14 | 0.5512 |
| M16 × 1.5 | 1.5 | Fine | 14.5 | 14.5 | 0.5709 |
| M18 × 2.5 | 2.5 | Coarse | 15.5 | 15.5 | 0.6102 |
| M18 × 1.5 | 1.5 | Fine | 16.5 | 16.5 | 0.6496 |
| M20 × 2.5 | 2.5 | Coarse | 17.5 | 17.5 | 0.6890 |
| M20 × 1.5 | 1.5 | Fine | 18.5 | 18.5 | 0.7283 |
| M22 × 2.5 | 2.5 | Coarse | 19.5 | 19.5 | 0.7677 |
| M22 × 1.5 | 1.5 | Fine | 20.5 | 20.5 | 0.8071 |
| M24 × 3 | 3 | Coarse | 21 | 21 | 0.8268 |
| M24 × 2 | 2 | Fine | 22 | 22 | 0.8661 |
Thread pitch: threads per inch to millimetres
| TPI | Pitch (mm) | Metric pitch (mm) | TPI equivalent |
|---|---|---|---|
| 4 | 6.3500 | 0.25 | 101.60 |
| 5 | 5.0800 | 0.35 | 72.57 |
| 6 | 4.2333 | 0.4 | 63.50 |
| 7 | 3.6286 | 0.45 | 56.44 |
| 8 | 3.1750 | 0.5 | 50.80 |
| 9 | 2.8222 | 0.6 | 42.33 |
| 10 | 2.5400 | 0.7 | 36.29 |
| 11 | 2.3091 | 0.75 | 33.87 |
| 12 | 2.1167 | 0.8 | 31.75 |
| 13 | 1.9538 | 1 | 25.40 |
| 14 | 1.8143 | 1.25 | 20.32 |
| 16 | 1.5875 | 1.5 | 16.93 |
| TPI | Pitch (mm) | Metric pitch (mm) | TPI equivalent |
|---|---|---|---|
| 18 | 1.4111 | 1.75 | 14.51 |
| 20 | 1.2700 | 2 | 12.70 |
| 24 | 1.0583 | 2.5 | 10.16 |
| 28 | 0.9071 | 3 | 8.47 |
| 32 | 0.7938 | 3.5 | 7.26 |
| 36 | 0.7056 | 4 | 6.35 |
| 40 | 0.6350 | 4.5 | 5.64 |
| 48 | 0.5292 | 5 | 5.08 |
| 56 | 0.4536 | 5.5 | 4.62 |
| 64 | 0.3969 | 6 | 4.23 |
| 72 | 0.3528 | 8 | 3.18 |
| 80 | 0.3175 | 10 | 2.54 |
Sources for this chart
Number and letter drill diameters are transcribed from ASME B94.11M and cross-checked against a second published table; fractional sizes, millimetres and the percentage of thread are calculated.
- ASME B94.11M — Twist drills: number, letter, fractional and metric sizes
- ASME B1.1 — Unified inch screw threads (UN and UNR thread form): UNC and UNF series
- ISO 261 and ISO 262 — ISO general-purpose metric screw threads: diameter and pitch combinations
- ISO 2306 / DIN 336 — Drills for use prior to tapping screw threads
- Machinery's Handbook — Percentage of thread: n × (major diameter − drill) ÷ 0.01299
- International Yard and Pound Agreement (1959) — 1 in = 25.4 mm exactly
Related Converters & Charts
Drill Size Chart and Tap Drill Chart FAQs
Common questions about the drill size chart.
What size drill for a 1/4-20 tap?
A #7 drill (0.201 in, 5.11 mm) gives about 75% thread for 1/4-20 UNC. For 1/4-28 UNF use a #3 drill (0.213 in).
What is the tap drill size for M8?
For M8 × 1.25 coarse thread, the tap drill is the major diameter minus the pitch: 8 − 1.25 = 6.75 mm, usually drilled 6.8 mm. M8 × 1 fine uses a 7 mm drill.
How big is a #29 drill?
A #29 drill is 0.1360 in (3.454 mm). It is the tap drill for #8-32 UNC and #8-36 UNF screws.
Can I download this chart as a PDF, CSV, or JSON?
Yes. Use the Download A4 PDF or US Letter PDF buttons for a printable version, or download the same tables as CSV or JSON from the links on this page.